India’s EPR & Plastic Packaging Rules in 2026: How Sustainable PET Packaging Supports Compliance – Part 2

As India’s packaging regulations continue to evolve, businesses are increasingly shifting toward sustainable packaging solutions that support compliance, recyclability, and circular economy goals.

For brand owners, packaging is no longer only about product protection and aesthetics; it has become a critical part of sustainability strategy and regulatory readiness.

With increasing focus on recycled content usage, recyclable packaging structures, and responsible waste management, PET and rPET packaging are playing a major role in helping businesses align with India’s evolving EPR framework.

Growing Focus on Recycled Content Usage

India is encouraging the use of recycled plastic content in packaging, especially in rigid plastic applications such as PET bottles and containers.

As per the latest guidelines, the use of recycled content (PCR – Post-Consumer Recycled material) in plastic packaging has been made mandatory for brand owners as part of the Government’s continued focus on sustainability, circular economy practices, and plastic waste reduction.

Brand owners are now required to ensure compliance with prescribed minimum recycled content percentages across applicable packaging categories. This makes it increasingly important for businesses to review existing packaging specifications and prepare for timely PCR integration.

The growing adoption of rPET (Recycled PET) helps:

  • Reduce dependence on virgin plastic
  • Support circular packaging systems
  • Lower carbon footprint
  • Improve sustainability performance
  • Align with evolving compliance requirements

As industries move toward higher recycled content adoption, reliable sourcing, quality assurance, and regulatory compliance will become critical factors in packaging decisions.

Why PET Packaging Continues to Be a Preferred Choice

PET continues to remain one of the most preferred packaging materials due to its

  • High recyclability
  • Lightweight structure
  • Durability
  • Cost efficiency
  • Strong circular economy potential

With advancements in recycling infrastructure and food-grade rPET processing technologies, PET packaging is helping businesses transition toward more sustainable and regulation-compliant packaging solutions.

The increasing adoption of recyclable and recycled-content PET packaging is expected to play a major role in India’s packaging industry transformation in the coming years.

Sustainable Packaging Design Is Becoming Essential

Packaging design now plays a critical role in both recyclability and regulatory compliance.

Many businesses are actively shifting toward:

  • Lightweight packaging solutions
  • Recyclable PET packaging
  • Mono-material structures
  • Optimized packaging designs
  • Reduced material consumption

Efficient packaging design not only supports sustainability goals but also improves transportation efficiency and overall operational performance.

Supporting the Transition Toward PCR Integration

As compliance requirements continue to evolve for FY 2026–27 and beyond, proactive planning and early adoption of recycled-content packaging will play a key role in ensuring long-term business readiness.

At Chemco Group, we are fully equipped to support this transition through our advanced RPET manufacturing capabilities. Our RPET production line is FSSC approved and aligned with applicable regulatory and quality standards, enabling us to support brands with sustainable and compliant packaging solutions.

We continue to collaborate with customers for:

  • PCR integration planning
  • Product development and trials
  • Sustainable packaging transition
  • Supply of high-quality recycled material tailored to application requirements

Moving Toward a Circular Packaging Economy

India’s packaging sector is entering a transformative phase where innovation, sustainability, and compliance are becoming deeply interconnected.

As regulations continue to evolve, collaboration between brand owners, packaging manufacturers, recyclers, and policymakers will be essential for creating scalable and sustainable packaging ecosystems.

Businesses that proactively invest in recyclable packaging, recycled content integration, and efficient waste management systems will be better positioned to meet future regulations while strengthening consumer trust and long-term competitiveness.

Conclusion

The shift toward sustainable packaging is no longer a future trend — it is becoming an industry-wide necessity. As India strengthens its EPR and recycled-content regulations, businesses must align their packaging strategies with circular economy goals and evolving compliance requirements.

PET and rPET packaging solutions offer significant opportunities for brands to improve sustainability performance, reduce environmental impact, and build future-ready packaging systems.

At Chemco Group, we remain committed to supporting brands with innovative, recyclable, and sustainability-focused packaging solutions designed to meet the changing needs of modern industries and environmental regulations.
What Brand Owners Must Know About India’s EPR & Plastic Packaging Rules in 2026 – Part 1

As India moves toward a more sustainable and circular economy, packaging regulations are becoming stricter and more structured than ever before. For brand owners across FMCG, food & beverage, personal care, pharmaceutical, and industrial sectors, understanding Extended Producer Responsibility (EPR) and plastic packaging regulations is no longer optional; it is a critical business requirement.

With evolving compliance mandates, increasing sustainability expectations, and stronger enforcement mechanisms, businesses must proactively prepare for the future of responsible packaging.

Understanding Extended Producer Responsibility (EPR)

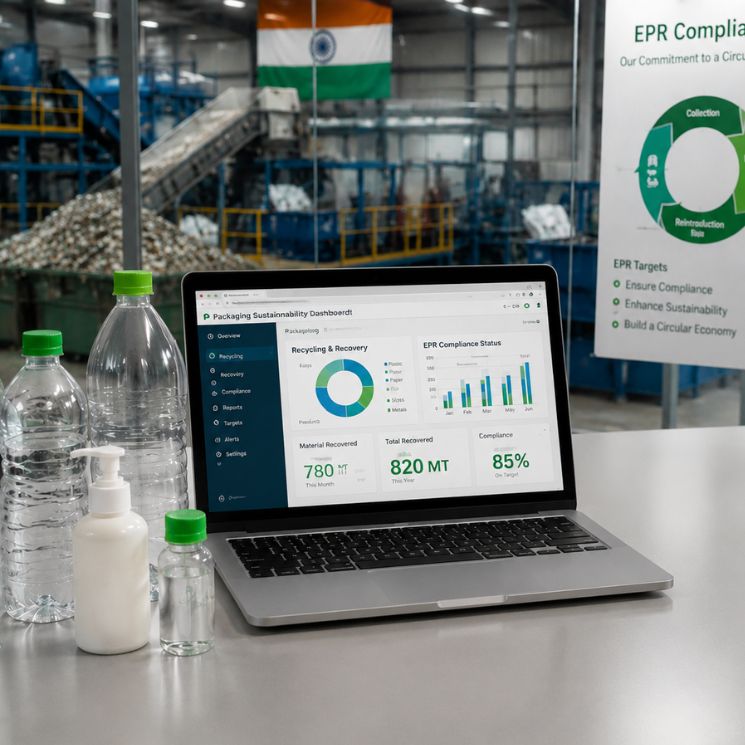
Extended Producer Responsibility (EPR) is a government-led framework under India’s Plastic Waste Management Rules that makes Producers, Importers, and Brand Owners (PIBOs) responsible for the collection, recycling, and environmentally sound management of plastic packaging introduced into the market.

The primary objective of EPR is to strengthen plastic waste management systems, improve recycling rates, and reduce environmental impact through a more circular packaging ecosystem.

For businesses, this means packaging responsibility now extends beyond manufacturing and distribution; it also includes post-consumer waste management.

Why EPR Compliance Is Becoming More Important in 2026

India’s packaging industry is witnessing a major regulatory shift driven by sustainability goals and environmental accountability. In 2026, stricter implementation and monitoring of plastic waste management rules are expected across industries.

For brand owners, non-compliance can lead to:

  • Regulatory penalties
  • Operational disruptions
  • Challenges in market expansion
  • Increased scrutiny from retailers and export markets
  • Negative impact on brand reputation

At the same time, businesses investing in sustainable packaging and recycling initiatives are building stronger consumer trust and long-term competitiveness.

Key Plastic Packaging Rules Brand Owners Must Know

Mandatory EPR Registration

All Producers, Importers, and Brand Owners dealing with plastic packaging are required to register on the Central Pollution Control Board (CPCB) EPR portal.

Without proper registration and reporting, businesses may face compliance-related restrictions and legal challenges.

Recycling & Collection Targets

Companies are required to ensure that an equivalent quantity of plastic packaging introduced into the market is collected and processed through authorized recycling or waste management channels.

The government continues to increase recycling obligations gradually to improve plastic recovery and reduce landfill dependency.

This has made partnerships with authorized recyclers and sustainable packaging manufacturers increasingly important.

Importance of Traceability & Documentation

Regulatory compliance now requires better transparency and documentation throughout the packaging lifecycle.

Businesses are expected to maintain proper records related to:

  • Packaging material introduced into the market
  • Waste collection and recycling certificates
  • Authorized recycler partnerships
  • Recycled content utilization

Digital tracking and reporting systems are becoming essential for smooth EPR compliance management.

Preparing for the Future of Responsible Packaging

For modern businesses, EPR compliance should not be viewed only as a legal obligation. It is an opportunity to strengthen sustainability strategies, improve packaging efficiency, and build long-term brand value.

Brand owners who proactively adapt to evolving packaging regulations today will be better positioned to:

  • Meet future compliance requirements
  • Build stronger consumer trust
  • Improve sustainability performance
  • Strengthen retailer and export partnerships
  • Enhance overall business resilience

Conclusion

India’s packaging industry is entering a new phase where sustainability, compliance, and accountability are becoming deeply interconnected. As regulations continue to evolve, businesses must take proactive steps toward responsible packaging practices and stronger waste management systems.

Understanding EPR requirements today will help brand owners build future-ready operations while improving long-term sustainability performance and market competitiveness.

In Part 2, we explore how sustainable PET packaging, recycled content integration, and circular packaging strategies can help brands meet evolving EPR goals and future compliance requirements.

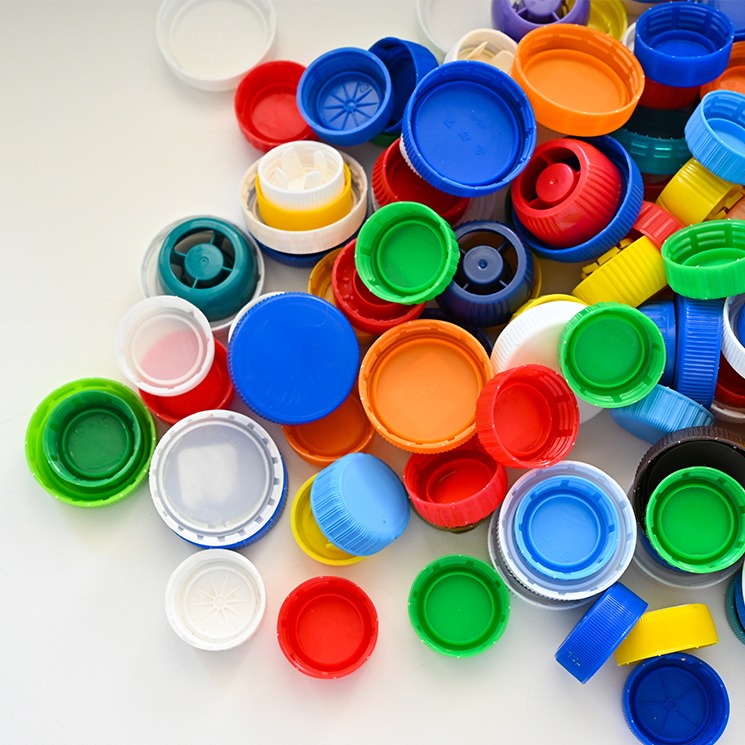
How Caps and Closures Affect Leakage Control, Tamper Evidence and Consumer Experience

In packaging, caps and closures are often treated as small components within a much larger system. In reality, they carry significant functional responsibility. A bottle or container can be well designed, visually strong, and suitable for the product, but if the closure does not perform consistently, the pack is compromised. Leakage, poor sealing, weak tamper evidence, and a poor opening experience can all undermine product quality and brand trust.

For packaging manufacturers and brand owners, caps and closures are not a finishing detail. They are a critical part of pack performance. Their design, fit, and application directly influence product protection, supply chain reliability, and how the consumer experiences the product from the first use onwards.

Leakage control starts with closure precision

One of the primary roles of any closure is to seal the pack effectively. If that seal is inconsistent, the consequences are immediate. Leakage results in product loss, transit damage, rejected inventory, retailer complaints, and avoidable cost across the supply chain.

This is why closure performance begins with dimensional precision. The thread profile, sealing surface, closure geometry, and fit with the container neck must all be engineered correctly. Even minor variation in cap dimensions can affect sealing performance, particularly on high-speed filling lines where consistency is essential.

A reliable closure must perform under filling pressure, stacking load, handling stress, and changing storage conditions. In liquid packaging especially, leakage control depends not just on the container, but on how accurately the cap is moulded, applied, and maintained throughout distribution.

Application torque has a direct impact on pack integrity

Torque is one of the most important factors in closure performance. If a cap is applied too loosely, seal integrity can be lost. If it is applied too tightly, the closure may become difficult to open or create thread stress that affects pack performance.

From a manufacturing standpoint, torque control is a quality parameter, not simply a machine setting. It needs to be managed carefully to ensure closures are secure enough to protect the product while remaining practical for the end user. This becomes particularly important in categories where packs are opened and reclosed multiple times.

Well-designed caps and closures support repeatable application on the production line and consistent opening performance in the market. That balance is essential to both operational efficiency and consumer satisfaction.

Tamper evidence strengthens consumer trust

Tamper evidence is now a basic expectation in many packaging categories. Consumers want reassurance that the product they are purchasing has not been opened or interfered with. Caps and closures play a central role in providing that reassurance.

Tamper-evident closures are designed to give a clear indication of first opening. When this is executed well, it supports both compliance and confidence. When it is poorly designed or inconsistently manufactured, it can create uncertainty at the point of purchase.

For brands, this matters because packaging is part of the trust equation. A closure that gives a visible and reliable indication of pack integrity helps reinforce product credibility. It shows that product safety and packaging discipline have been taken seriously.

Consumer experience is shaped by closure performance

The consumer does not interact with a packaging specification. They interact with the cap or closure, and that moment matters more than many businesses realise. If the closure is difficult to open, uncomfortable to grip, prone to dribbling, or unable to reclose properly, the overall product experience suffers.

This is where functionality becomes commercially important. A closure must not only seal well, but also perform smoothly in everyday use. Opening force, grip design, pour control, and reclosure all influence how the pack is perceived. A poor closure experience can make even a good product feel inconvenient or poorly designed.

In this sense, the cap becomes part of the brand experience. Consumers may not comment on thread design or torque retention, but they will notice when a closure works well and when it does not.

Manufacturing consistency is critical

Closure performance depends heavily on moulding precision and process control. Material selection, tooling accuracy, shrinkage management, and dimensional consistency all affect how the final part performs. A closure that looks acceptable visually may still create sealing or application issues if tolerances are not well controlled.

For packaging manufacturers, this places the focus on disciplined production. High-quality caps and closures require reliable moulding conditions and a clear understanding of end-use requirements. The closure must perform not only in isolation, but as part of a complete packaging system under real operating conditions.

This is particularly important where pack performance affects shelf life, product hygiene, or repeated consumer use. A technically sound closure contributes to long-term packaging reliability.

Small component, major impact

Caps and closures may be among the smallest parts of a packaging format, but they have a direct effect on product protection, line performance, and user confidence. Their value is often underestimated because they are expected to work without drawing attention. When they fail, however, the impact is immediate and highly visible.

For that reason, closure selection should not be based only on unit cost. It should be assessed in terms of sealing reliability, tamper evidence, manufacturing consistency, and user experience. These are the factors that determine whether the pack performs well in the market and across the supply chain.

Conclusion

Caps and closures do far more than complete a pack. They are central to leakage control, tamper evidence, and the consumer’s experience of the product. A well-engineered closure protects product integrity, supports production efficiency, and gives the user confidence every time the pack is opened and reclosed.

For packaging businesses, the message is clear. Closure performance is not a minor detail. It is a technical and commercial requirement that directly affects packaging quality and brand trust

Primary, Secondary and Transit Packaging: What Each Layer Must Deliver

Packaging is often discussed as a single function, but in practice it operates as a system. From the point of filling to the point of sale and through to final delivery, different packaging layers perform different roles. Primary packaging, secondary packaging, and transit packaging each carry specific responsibilities, and the overall efficiency of the supply chain depends on how well those layers work together.

For manufacturers and brand owners, this is not just a design matter. It is an operational decision that affects product protection, line efficiency, storage, transport, retail presentation, and customer experience. When one layer underperforms, the entire packaging system feels the impact.

Primary Packaging Must Protect the Product and Support Use

Primary packaging is the layer that comes into direct contact with the product. In sectors such as food, beverages, personal care, pharmaceuticals, and household products, this is the most critical packaging interface. It must protect product integrity, preserve shelf life, maintain hygiene standards, and provide ease of use for the consumer.

The expectations from primary packaging are both technical and commercial. It needs to offer barrier performance where required, maintain dimensional consistency on filling lines, support closure fitment, and deliver a reliable pack structure through storage and handling. At the same time, it must also support brand presentation on shelf.

In practical terms, primary packaging must do three things well. It must keep the product safe, run efficiently in production, and remain functional in the hands of the end user. If it fails in any one of these areas, the cost is immediate, whether through leakage, contamination, rejection, or brand damage.

Secondary Packaging Must Group, Protect and Present

Secondary packaging sits around the primary pack. Its role is to group units together, improve handling, add another layer of protection, and support merchandising or distribution requirements. This includes formats such as cartons, shrink bundles, sleeves, trays, and wrap-around solutions depending on the product category and route to market.

Strong secondary packaging helps create order in the supply chain. It allows primary packs to move as consolidated units, improves ease of stacking, and reduces the risk of damage during internal movement and retail handling. It can also play a significant role in shelf-ready presentation, especially in modern trade environments where replenishment speed and pack visibility matter.

From a manufacturing perspective, secondary packaging must also be machine compatible and structurally stable. It should support efficient packing operations without creating unnecessary complexity. A well-designed secondary pack reduces handling inefficiencies and protects the primary pack from avoidable stress before it reaches the consumer.

Transit Packaging Must Withstand Movement Across the Supply Chain

Transit packaging is the outermost packaging layer used for warehousing, palletisation, transport, and distribution. Its job is straightforward but demanding. It must protect the packaged goods through stacking, loading, unloading, long-distance transport, and changing storage conditions.

This is where transit packaging becomes a serious supply chain tool rather than a simple outer cover. It must deliver compression strength, load stability, impact resistance, and handling efficiency. Stretch wrap, shrink film, corrugated boxes, pallet covers, and other transport-oriented materials all fall into this category depending on the movement requirement.

A failure at the transit stage can erase the value created by the inner packaging layers. Even if the primary and secondary packaging are well engineered, poor transit protection can still result in crushed packs, leakage, scuffing, contamination, or product loss. That is why transit packaging should be evaluated in line with route conditions, storage patterns, shipping distances, and pallet configuration rather than treated as an afterthought.

Each Layer Has a Different Job, but They Must Work as One System

One of the most common mistakes in packaging development is assessing each layer in isolation. In reality, packaging performs best when all three layers are developed as part of one integrated system. The primary pack must suit the product and production line. The secondary pack must support handling and grouping. The transit pack must protect the load through the distribution chain.

When these layers are aligned, the business benefits are clear. Filling lines run more smoothly. Damage rates stay lower. Warehousing becomes more efficient. Transport loads become more stable. Retail handling improves. The product reaches the market in better condition and at lower operational cost.

This systems approach is especially important for high-volume sectors where even small improvements in pack performance can influence total supply chain economics. Packaging decisions should therefore be based not only on material cost, but on total delivered value.

Performance, Efficiency and Practicality Must Be Balanced

Every packaging layer brings trade-offs. Stronger materials may improve protection but add cost or weight. More visually appealing secondary formats may improve shelf presence but reduce packing speed. Lighter transit solutions may save material but increase the risk of transport damage if not properly engineered.

The right packaging strategy balances these factors with a clear view of product requirements, distribution conditions, and commercial priorities. That is why businesses increasingly look for packaging partners who understand not just individual components, but the full packaging architecture.

In industrial terms, the goal is simple. Each layer must perform its role without creating inefficiency for the next stage. Good packaging is not only about containment. It is about convertibility, stackability, transport stability, and consistent delivery across the supply chain.

Packaging Performance Should Be Measured Across the Full Journey

The effectiveness of packaging cannot be judged only at the filling line or only at the point of sale. It needs to be assessed across the entire product journey. That includes machine performance, storage conditions, transport stress, retail handling, and end-user interaction.

For this reason, packaging protection should be measured across all three levels. Primary packaging must protect the product itself. Secondary packaging must support grouping and handling. Transit packaging must protect the load in motion. Each level adds a layer of assurance, and each one contributes to overall supply chain reliability.

Conclusion

Primary packaging, secondary packaging, and transit packaging each serve a distinct purpose, but none of them can be treated in isolation. Together, they determine how well a product is protected, handled, transported, displayed, and delivered.

For brands and manufacturers, the priority should not be to optimise one layer at the expense of the others. It should be to build a packaging system in which every layer delivers what the next stage needs. That is how packaging moves from being a cost centre to becoming a performance driver across production, logistics, and market execution.

From Collection to Reprocessing: What Determines the Quality of Recycled PET

As demand for recycled PET continues to grow, the conversation is moving beyond recycled content targets and towards material quality. In the packaging industry, that distinction matters. Using rPET made from post-consumer PET bottles is not simply about recovering waste. It is about producing a recycled resin stream that is stable, processable, and suitable for new packaging applications.

The quality of rPET bottles begins long before reprocessing. It starts with how used PET bottles are collected, handled, sorted, washed, and converted into flakes or pellets. Every stage in that chain affects the final output. For converters and brand owners, understanding this is essential because poor-quality recycled material can create challenges in preform moulding, blow moulding, clarity, colour consistency, and food-contact compliance.

Collection Quality Sets the Starting Point

The quality of recycled PET is heavily influenced by the quality of the incoming bottle stream. If collection systems deliver PET bottles that are heavily mixed with other plastics, metal, paper, food residue, or non-recyclable waste, the recycler begins with a disadvantage. A clean, well-segregated collection stream improves both yield and final resin quality.

In practical terms, bottle-to-bottle recycling works best when PET bottles are collected with minimal contamination and sorted early in the chain. The more mixed the feedstock, the more difficult and expensive it becomes to recover high-quality material. For the recycling industry, collection efficiency is not just an environmental issue. It is the first quality control point.

Sorting Accuracy Has a Direct Impact on rPET Performance

Once collected, used PET bottles must be sorted correctly. This stage is critical because recycled PET intended for packaging cannot carry excessive contamination from PVC, polyolefins, coloured bottles, labels, caps, adhesives, or foreign materials. Even small levels of incompatible material can affect the performance of the recycled output.

Sorting technology and process discipline play a major role here. Near-infrared sorting, colour separation, metal removal, and manual quality checks all help improve feedstock purity. Clear PET bottle streams are particularly valuable because they provide greater flexibility in reprocessing and support higher quality end applications. Poor sorting, by contrast, reduces the consistency of the recycled resin and limits where it can be used.

Contamination Control Is Central to Recycled PET Quality

In bottle-to-bottle recycling, contamination is one of the biggest determinants of material quality. Contamination can come from product residue inside bottles, dirt and moisture during storage, mixed polymers, multilayer packaging, shrink sleeves, labels, adhesives, and closure components.

If these contaminants are not removed effectively, they can affect intrinsic viscosity, colour, odour, acetaldehyde levels, and process stability during remanufacturing. For converters, this may result in black specks, haze, inconsistent melt behaviour, or rejection on the production line. For food and beverage applications, contamination control becomes even more important because the recycled material must meet stricter safety and compliance expectations.

Washing and Flake Preparation Determine Process Readiness

After sorting, the bottles move into washing and size reduction. This stage is often underestimated, but it has a direct effect on the final usability of the material. Effective hot washing, friction washing, rinsing, and drying are required to remove residues, glue, paper, fines, and other surface contaminants before the PET is turned into clean flakes.

High-quality PET bottle recycling depends on producing flakes with consistent size, low moisture, low contamination, and stable bulk characteristics. Flake quality matters because it determines how the material behaves in downstream reprocessing. If the flakes are inconsistent or poorly cleaned, that problem carries forward into extrusion, pelletising, and eventually into packaging conversion.

Intrinsic Viscosity and Thermal History Must Be Managed Carefully

One of the more technical factors affecting recycled PET quality is intrinsic viscosity, often referred to as IV. In simple terms, IV influences the strength and processability of PET during remanufacturing. Used bottles go through thermal and mechanical stress during their first life and then again during recycling. If that thermal history is not managed carefully, polymer degradation can reduce performance.

This is why decontamination, drying, extrusion control, and in some cases solid-state polycondensation are so important in the rPET process. These steps help restore or stabilise material properties so that the recycled PET can be used effectively in demanding packaging applications. For converters working with preforms and bottles, IV consistency is essential for stable processing and reliable pack performance.

Colour and Clarity Depend on Feedstock Discipline

For many packaging applications, especially beverages, the visual quality of rPET matters nearly as much as its mechanical performance. The colour and clarity of recycled PET are directly affected by the input bottle mix. A stream with high levels of coloured bottles, opaque PET, additives, or degraded material will produce a less clear recycled output.

That has commercial consequences. Brand owners want packaging that supports both sustainability objectives and shelf appeal. If the recycled resin has excessive yellowness, haze, or visual inconsistency, it becomes more difficult to use in premium applications. This is why disciplined bottle collection, accurate colour sorting, and controlled reprocessing are all essential to achieving high-quality food grade rPET.

Food-Grade Applications Require Stronger Decontamination Standards

When rPET is intended for direct food or beverage contact, the quality threshold becomes significantly higher. The recycling process must demonstrate that potential contaminants have been effectively removed and that the final material is suitable for safe use in packaging.

This requires more than standard mechanical recycling. It requires a controlled bottle-to-bottle process with validated decontamination, traceable input streams, and strict operating parameters. For packaging manufacturers, this is a critical point. Not all recycled PET is equal, and not every recycled stream is suitable for food-contact use. The ability to produce high-quality rPET from used PET bottles depends on both feedstock quality and process capability.

Reprocessing Quality Determines End-Use Value

The final stage is reprocessing the cleaned PET into usable raw material, typically flakes or pellets, for conversion into new packaging. At this point, the material must deliver consistency in melt behaviour, moisture control, colour profile, and contaminant limits. If it does, it can support reliable use in bottle to bottle recycling and other packaging formats. If it does not, its value drops and its application range becomes more limited.

For the industry, this is where the economics of recycling become clear. Higher quality input and stronger process control create a better recycled output, and better output supports higher-value end uses. In that sense, recycled PET quality is not determined by one machine or one stage alone. It is the result of discipline across the entire chain.

Conclusion

The quality of recycled PET made from used bottles is shaped by every step from collection to reprocessing. Clean collection streams, accurate sorting, effective contamination removal, strong washing systems, controlled IV management, and validated decontamination all play a role in determining whether rPET can perform in new packaging applications.

For brand owners, converters, and recyclers, the lesson is straightforward. High-quality rPET does not happen by default. It is built through system control, process consistency, and a clear understanding of what bottle-to-bottle recycling requires. As the market expects more recycled content in packaging, the companies that will lead are the ones that focus not only on quantity of recycled material, but on the quality that makes it commercially and technically viable.