
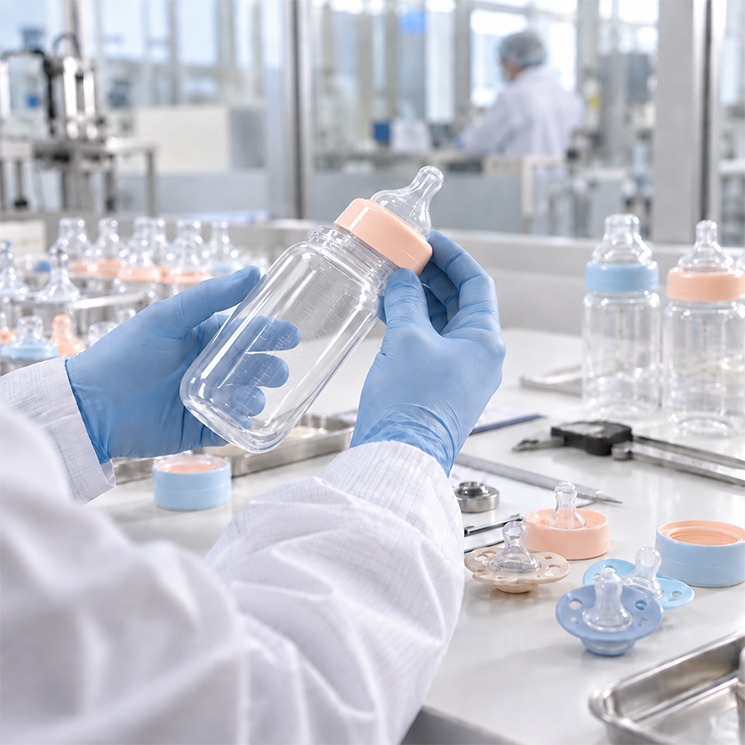
Launching a baby care brand is exciting, but turning an idea into a market-ready product involves more than choosing a design and finding someone to manufacture it.
There are decisions around materials, product design, moulds, manufacturing, testing, quality and packaging. And because baby care products are used by infants, these decisions need to be taken seriously from the very beginning.
This is where choosing the right contract manufacturing partner can make a difference.
A good manufacturing partner should do more than produce your product. They should understand your requirements, help you address manufacturing challenges and have the capabilities to support you as your brand grows.
Here are seven things to consider before choosing one.
1. Look Beyond Production Capacity
Having enough machines and production capacity is important, but it should not be the only thing you look at.
Baby care manufacturing can involve several stages, from product development and engineering to mould development, manufacturing, testing, assembly and packaging.
If you need a different supplier for every stage, managing the development process can become complicated.
Instead, look for a manufacturer who can support more of the product journey.
Ask:
- Can they support product development and customisation?
- Do they have engineering and tooling capabilities?
- What manufacturing technologies do they have?
- Can they manufacture different baby care components?
- Can they support higher volumes as your brand grows?
The right partner should understand not just how to produce the product, but also what it takes to produce it consistently.
2. Understand the Materials Being Used
Material selection is an important part of baby care product development.
A feeding bottle, nipple, soother or sipper may have very different functional requirements. The material needs to be selected based on the product’s design, application and intended use.
Before finalising a manufacturer, ask:
- What material will be used for each component?
- Is the material suitable for the intended application?
- What grade of material is being used?
- How is the raw material inspected?
- What documentation can be provided?
For example, Chemco uses virgin-grade polypropylene and USFDA-approved medical-grade Liquid Silicone Rubber (LSR) for its baby care products, depending on the application.
It is better to have these conversations early. Changing materials later can affect product design, moulds, processing and even production timelines.
3. Look Closely at Quality and Compliance
For baby care products, quality cannot be treated as something that happens only at the end of the production line.
A reliable manufacturing process should include checks at different stages, starting with raw materials and continuing through production and finished-product inspection.
When evaluating a manufacturer, ask how they manage:
- Raw material inspection
- Process controls
- In-process quality checks
- Product testing
- Batch traceability
- Internal audits
- Non-conforming products
You should also understand which standards and certifications apply to the product you are developing.
Chemco’s baby feeding bottles and nipples are certified to EN 14350:2020 requirements, and its baby feeding bottles and nipples have BIS 3565 certification. The facility also includes a dedicated laboratory for quality and product testing.
Instead of simply asking, “Are you certified?”, ask:
“Which standards does my product need to meet, and how do you maintain these requirements during production?”
That will give you a much better understanding of the manufacturer’s quality systems.
4. Don’t Underestimate the Importance of the Mould
When developing a new baby care product, it is easy to focus on the final product and overlook the mould behind it.
But mould design can have a direct impact on product dimensions, wall thickness, weight, component fit, surface finish and production consistency.
This becomes even more important when developing a customised product.
A manufacturer with engineering and tooling expertise should be able to identify potential manufacturing challenges before the mould is finalised.
For example, a design may look good on paper but create difficulties during production. Addressing such issues early is much easier than making changes after the mould has already been manufactured.
The earlier the manufacturer is involved, the easier it is to identify and solve these challenges.
5. Ask What Happens Between the First Sample and Mass Production
Getting one good sample is not the same as consistently manufacturing thousands of products.
This is an important difference to consider when choosing a contract manufacturer.
During development, you may go through several rounds of sampling before the final design is approved. But once production starts, the focus shifts to maintaining the same quality across every batch.
Ask your manufacturer:
- What testing is carried out during development?
- What checks are performed during production?
- How are dimensions and weight controlled?
- How is product consistency monitored?
- What happens if a product does not meet the required specifications?
The objective should be simple: the product you receive in your next production batch should perform and look like the one you approved.
6. Think Beyond Manufacturing
Your product does not necessarily go straight from the production line to the customer.
Depending on your business model, you may also need assembly, printing, labelling and packaging.
Having these capabilities with the same manufacturing partner can make the overall supply chain easier to manage.
Chemco’s baby care capabilities include manufacturing, assembly, multi-colour pad and screen printing and packaging. Its facility also includes dedicated storage and controlled production areas.
This does not mean that every brand needs one supplier to handle everything. But understanding the complete range of services available can help you decide how you want to structure your supply chain.
7. Choose a Partner That Can Grow With Your Brand
Your manufacturing requirements can change considerably as your brand grows.
You may start with one feeding bottle and eventually introduce different sizes, nipples, sippers, soothers or other baby care products.
That is why scalability is worth discussing before you sign an agreement.
Look at:
- Current production capacity
- Minimum order quantities
- Lead times
- Available manufacturing technologies
- Ability to increase production volumes
- Quality systems at higher volumes
- Ability to develop additional products
A manufacturer that works well for your first order may not necessarily be the right partner when your volumes increase.
Ideally, you want a partner who can support both your launch and your next stage of growth.
What Should You Ask a Baby Care Contract Manufacturer?
Before making a decision, it can help to compare manufacturers using the same set of questions.
Product Development
Can you support product development and customisation?
Materials
What materials and grades are available for our application?
Tooling
Who will manage mould development and modifications?
Manufacturing
What technologies and production capabilities do you have?
Quality
What quality checks are carried out during production?
Compliance
Which applicable standards and certifications does the product meet?
Testing
What testing facilities are available?
Finishing
Can you support printing, assembly and packaging?
Scalability
Can you support higher production volumes as our brand grows?
The answers can help you understand whether you are simply choosing a supplier or building a longer-term manufacturing relationship.
The Chemco Perspective
At Chemco, we believe baby care manufacturing starts well before the production line.
Product design, material selection, tooling, manufacturing, quality control and packaging all play a role in developing a consistent, market-ready product.
Chemco has been working with baby care brands for over 30 years and offers manufacturing support across feeding bottles, nipples, soothers and pacifiers, sippers and training sets, breast pumps and other baby care accessories.
The facility includes dedicated raw material and finished goods storage, controlled production areas, cleanrooms, testing facilities and specialised equipment for different baby care components.
For a new or growing baby care brand, the right contract manufacturing partner can help make product development more structured, production more consistent and scaling easier.
Because ultimately, choosing a manufacturer is not just about where your product is made.
It is about the expertise, processes and quality systems behind every product that reaches a customer.